If you’re in the industrial parts manufacturing game, you know a face grinding machine isn’t just a piece of equipment—it’s the backbone that keeps your precision tolerances tight and your production lines moving. As a supplier who’s spent 12 years repairing, calibrating, and selling these machines to shops from small jobbing outfits to large automotive component factories, I’ve seen firsthand how lazy, reactive maintenance turns a $80,000 workhorse into a $10,000 paperweight faster than you can say “tolerance drift.” I’ve had shops call me at 2 a.m. after a machine seized mid-run because they skipped a weekly filter change, and another that cut their annual service costs by 62% just by sticking to a simple, consistent routine. This post isn’t some generic tech manual regurgitated from a manufacturer’s pamphlet—it’s the stuff I scribble in my service notebook at 7 a.m. before hitting the road, the tricks I’ve learned fixing machines that were mistreated by teams that thought “maintenance” was just calling someone when it broke. Let’s break down exactly how to keep your face grinder running like it did the day you uncrated it, no fancy certification needed. Face Grinding Machine
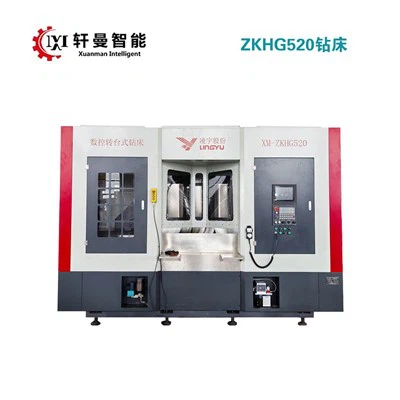
First, let’s get one thing straight: face grinders are picky, but they’re not complicated. Their main job—abrasively grinding a flat surface (often a face of a bearing, gear, or valve seat) to ultra-tight tolerances, usually within 0.001mm—relies on three core systems: the spindle (that spinning shaft holding the grinding wheel), the hydraulic/linear motion system that moves the table or wheel head, and the coolant/lubrication loop that keeps every moving part from welding itself together. Mess up any one of these, and you’re looking at part rejection, downtime, or worse—spindle damage that costs more than a third of a new used machine. I’ve seen a shop run their spindle 200 hours without a bearing check; by the time they called me, the runout was at 0.02mm, and the wheel had chewed up 50 batches of brake rotor faces that had to be scrapped. That’s $15,000 in bad parts alone, all because they skipped a 5-minute check.
Let’s start with the unsung hero: the coolant system. This is the biggest culprit of premature wear, hands down. Coolant isn’t just water or a mix of oil and water—it’s your machine’s blood, flushing away metal shavings, preventing thermal warping of the part being ground, and lubricating the grinding wheel’s grit so it doesn’t glaze over. I get at least three calls a month from shops where the coolant turned into a rancid, sludgy mess, clogging filters, gumming up the spindle, and causing wheel imbalance. Here’s the routine I preach, no exceptions: every single shift, check the coolant level on the machine’s sight glass. If it’s below the minimum mark, top it off with the correct mix (usually a 5-10% synthetic or semi-synthetic coolant, not straight tap water—tap water has minerals that cause scaling). Every 40 hours of operation, I want you to take a 10-minute break to skim the surface of the coolant tank with a fine mesh skimmer. That floating gunk is metal fines and dead bacteria, and if you leave it, it’ll sink and clog your inline filter. Most importantly, change the entire coolant and deep-clean the tank every 200 hours, not 500 like some lazy schedules say. I learned this the hard way: a shop once ran their coolant for 600 hours, and when I dropped the tank, there was a 2-inch layer of compacted metal sludge on the bottom. It had worked its way up into the spindle’s cooling jacket, causing it to overheat during high-speed grinding, and the resulting thermal expansion threw their tolerance off for two weeks. Pro tip: when you refill the tank, add a small amount of coolant biocide (follow the manufacturer’s dosage—too much will corrode seals, too little and bacteria grows) to prevent that slime buildup. Also, don’t forget the filters: your inline coolant filter should be changed every 80 hours, and the paper filter in the return line every 120 hours. Clogged filters mean no coolant flow, which means your wheel overheats, glazes, and starts burning parts. I’ve seen shops try to skip filter changes by backflushing them once a month, but in my experience, that only buys you 10 more hours before they’re so clogged they rupture, sending sludge straight to the spindle.
Next up, the spindle—your face grinder’s precision heart. The spindle is what holds the grinding wheel and spins it at 1,000 to 10,000 RPM, and its runout (the amount it wobbles) is what determines how flat your ground parts are. Most face grinders have precision roller or ball bearings in the spindle, and these bearings need consistent lubrication to survive. The first rule for spindles: never run them low on oil. If your spindle uses a recirculating oil system, check the oil level daily; if it’s a grease-lubricated spindle (common on smaller, lighter face grinders), check the grease fitting every shift. I always recommend using the manufacturer’s specified lubricant—don’t swap in a cheaper, thicker grease to “protect” the bearings. That’s a recipe for overheating. Once every 150 hours, you need to check the spindle runout. You can do this with a simple dial indicator (I keep a 0.001mm dial indicator in my service truck at all times) mounted on the machine’s table, touching the spindle’s outer shaft. Spin the spindle by hand (make sure it’s powered off!) and check the reading. If the runout is more than 0.002mm for high-precision grinders (used for aerospace or medical parts) or 0.005mm for general industrial parts, it’s time to either adjust the bearings or schedule a service—don’t wait until it’s 0.01mm, by which time the bearings are worn beyond repair and need replacing. Another big spindle mistake: letting coolant get into the spindle’s bearing cavity. Most modern spindles have seals to prevent this, but old or poorly maintained seals will fail over time. If you notice coolant leaking from the spindle’s lower end, shut the machine down immediately—coolant mixed with bearing oil is a death sentence for the bearings, and you’ll be replacing them before you know it. I once got a call from a shop that had a $120k face grinder with a coolant leak; they ran it for three shifts before I saw it. The bearings were already rusted, and the spindle had to be pulled, rebuilt, and rebalanced, costing them $40k and three weeks of downtime. Don’t be that guy.
Now, the linear motion and table system—this is what moves the grinding wheel across the part, and any slop or wear here will show up as uneven, wavy surfaces on your workpieces. The table and guide rails need to be kept clean and lubricated at all times. Every day, before the first run, take a lint-free cloth and wipe down the guide rails and the table’s surface. Metal shavings and coolant residue act like sandpaper, scratching the rails and causing stick-slip motion (that jerky movement when the table starts moving). Once every 80 hours, apply the correct lubricant to the guide rails—most face grinders use a way oil, not general machine oil, because way oil is formulated to prevent stick-slip. If your machine has ballscrews (common in CNC face grinders), those need to be lubricated every 100 hours as well. For manual face grinders, I see a lot of shops skip greasing the leadscrew, which eventually seizes up, making the table impossible to move. If you run a CNC grinder, don’t forget to calibrate the axis positions every 200 hours—thermal expansion from long runs can throw your coordinates off, leading to parts that are too thick or too thin. A quick calibration of the X and Z axes with a step gauge takes 15 minutes, and it prevents a lot of scrap. Also, check the table’s clamping mechanism every shift—loose clamps can cause the table to shift mid-run, ruining a whole batch of parts. I had a customer last year who forgot to tighten the table clamps before running a valve seat; the table shifted 0.5mm mid-run, and he had to scrap 200 valve seats, costing him $8k. That’s all because of a 10-second check before starting.
Let’s talk about grinding wheels—they’re the consumable that’s the most mistreated part on any face grinder, and it directly ties into maintenance. A dull or improperly dressed wheel causes extra wear on the spindle, causes thermal damage to parts, and wastes hours of production. First, always use the correct wheel for the material you’re grinding—aluminum oxide for steel, silicon carbide for cast iron, diamond wheels for ceramics or carbide. Once every 40 hours, or whenever you notice the wheel starting to burn parts or produce a finish that’s not smooth, you need to dress the wheel. Dressing is the process of truing the wheel (making it perfectly round) and cleaning the abrasive grit so it doesn’t glaze over. I don’t mean grabbing a cheap diamond dresser from the hardware store—get a proper single-point diamond dresser rated for your wheel size. Dress the wheel at a slow feed rate, and make sure there’s plenty of coolant flowing during dressing to prevent heat buildup. After dressing, take a moment to check the wheel’s balance—even a slightly out-of-balance wheel will cause spindle vibration, which ruins runout and wears out bearings faster. For manual balancing, I use a dynamic balancing tool, and for CNC grinders, most modern machines have automatic balancing that takes 2 minutes once a shift. Another wheel tip: never run a wheel that’s cracked or chipped. Inspect the wheel visually before every use, and if you see any cracks, replace it immediately. A broken wheel can shatter at high RPM, which is an extreme safety hazard. I’ve had a shop where a chipped wheel shattered, sending a piece of shrapnel through the machine’s guard and nearly hitting an operator—they’re lucky no one was hurt.
I also can’t stress enough the small, daily checks that add up to huge savings. At the start of every shift, check all emergency stop buttons to make sure they engage properly—yes, even if they look fine, test them. You never know if a wire frayed over the weekend. Check all power cables and hydraulic hoses for cracks or fraying—old hoses can burst under pressure, causing fluid leaks or even fires. For CNC face grinders, check the machine’s error logs at least once a week—most of the time, error codes will give you a heads-up about a failing component before it causes a breakdown. Last year, a customer of mine noticed a minor over-temperature error code in his log, and when I checked, the spindle’s cooling fan was clogged with dust. We cleaned it, and he avoided a spindle overheat that would have cost him $30k in repairs and downtime. If you ignore error logs, they’re useless—treat them like a maintenance tool, not a nuisance.

Now, let’s address the elephant in the room: when to call in a professional. A lot of shops try to do all maintenance in-house, and that’s fine for the daily checks, but there are times when you need someone who knows these machines inside and out. Every 500 hours, schedule a full service: that’s pulling the spindle, inspecting the bearings, rebalancing it, checking the guide rail wear, and calibrating all axes. Don’t wait until the machine is acting weird—proactive service catches problems before they become disasters. I tell all my customers: the $1,500 annual service call saves you $15,000 in emergency repairs and scrap. It’s basic math.
Slant Bed Lathe Look, I’m not here to sell you a new machine or scare you into buying unnecessary parts. I’ve seen enough bad maintenance practices to know that most breakdowns are preventable. A face grinding machine is a precision tool, and it deserves the same attention you’d give a high-performance truck or a race car—consistent, small checks every day, instead of a big overhaul once a year. If you stick to the routine I laid out here, you’ll see lower part scrap rates, less downtime, and a longer lifespan for your machine. If you have questions about specific maintenance steps for your model of face grinder, or you’re looking to upgrade your equipment to reduce maintenance time and improve precision, don’t hesitate to reach out to our team for guidance. We work with shops of all sizes, and we’re here to help you keep your production running smoothly.
References
- Machine Tool Maintenance: A Practical Guide for Precision Machinists, Industrial Press Inc., 2019
- Guidelines for Face Grinder Coolant System Management, Association for Manufacturing Technology (AMT), 2021
- Spindle Maintenance and Calibration Standards for Precision Grinding, National Institute of Standards and Technology (NIST), 2020
- Safe and Effective Grinding Wheel Handling Practices, Occupational Safety and Health Administration (OSHA), 2022
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
We’re well-known as one of the leading face grinding machine manufacturers in China, featured by quality products and low price. Please rest assured to buy discount face grinding machine made in China here from our factory. We also accept customized orders.
Address: No. 1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-cnc.com/
